How to Choose Precision Injection Molding Suppliers in 2026?

Choosing a precision injection molding supplier in 2026 requires more than comparing unit prices. The right partner must understand material behavior, mold design, process control, and production risk. A capable supplier should prove these skills through documented results, not attractive promises.

In practical sourcing work, small details often expose larger problems. Ask for sample inspection reports, mold maintenance records, tolerance data, and traceability procedures. Review how the supplier controls temperature, pressure, cycle time, and visual defects. Their answers should be specific. Vague explanations deserve careful attention.

A factory tour can reveal important evidence. Look for clean production areas, calibrated measuring equipment, organized material storage, and operators who understand the process. Request references from projects with similar resins, part sizes, tolerances, and annual volumes. Certifications can support trust, but certificates alone do not guarantee consistent quality. No supplier is perfect. Our own early evaluations have sometimes focused too heavily on equipment and overlooked communication speed. That weakness can become expensive during tooling changes or urgent corrective actions.

A reliable supplier should also explain design-for-manufacturing decisions clearly. They need to discuss draft angles, gate locations, warpage control, cooling channels, and expected tool life. Commercial transparency matters as well. Confirm tooling ownership, inspection standards, lead times, warranty terms, and change-control procedures before signing an agreement.

This guide examines practical selection criteria for 2026. It connects technical evidence with real production needs, helping buyers compare suppliers fairly. The goal is not to find the cheapest factory. It is to find a dependable manufacturing partner that can deliver repeatable parts, honest communication, and measurable improvement over time.
How to Choose Precision Injection Molding Suppliers in 2026?

Define Precision Injection Molding Requirements

Before comparing precision injection molding suppliers, define what “precision” means for the part. State critical dimensions, acceptable tolerances, material grade, surface finish, and expected service temperature. Add datum references and measurement methods. A tolerance of ±0.02 mm means little without specifying temperature, gauge resolution, and inspection location.

Use functional data, not attractive sample parts. For example, specify cavity pressure limits, shrinkage assumptions, warpage allowance, and the required Cpk target. Many manufacturers use Cpk 1.33 as a practical process-capability benchmark for critical features. The ISO 20457 framework also separates general and special tolerances for molded plastic parts. That distinction should appear in the drawing. It reduces arguments later. Sometimes, a ±0.01 mm request looks impressive but adds cost without improving product performance.

Your requirement should also include volume, annual demand, cycle-time expectations, mold life, and inspection frequency. A 2024 market analysis by Fortune Business Insights estimated the injection molded plastics market at about USD 388 billion in 2023, showing the scale of competition and production capacity. Scale, however, does not prove precision. Request capability studies from actual production tools, dimensional reports from multiple lots, and evidence of calibrated equipment. Ask how the supplier controls resin drying, mold temperature, and cooling time. These details often decide whether a small connector fits after 100,000 cycles. I would also review the specification with a tooling engineer. Even experienced teams occasionally over-tolerate noncritical surfaces. That mistake is expensive.

Assess Supplier Capabilities and Production Equipment

How to Choose Precision Injection Molding Suppliers in 2026?

Assess Supplier Capabilities and Production Equipment

A reliable supplier should prove its capabilities with recent production data, not polished promises. Ask how it controls mold temperature, injection speed, holding pressure, and cooling time. These settings directly affect shrinkage, warpage, and part consistency. Request capability studies for critical dimensions, including Cp and Cpk results. Ask for evidence.

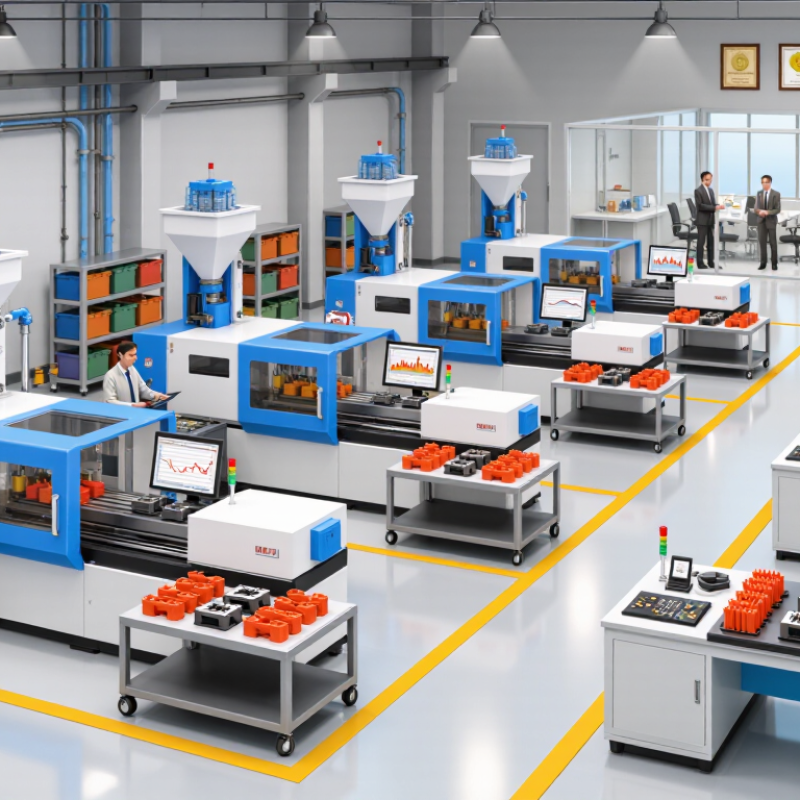
Walk through the production area, either in person or through a live video audit. Check whether molding machines match the required shot size, clamping force, and material type. Oversized equipment can waste energy and reduce control. Undersized equipment may create unstable filling. The right fit matters. Inspect dryers, material loaders, temperature controllers, and automated inspection systems. Clean equipment is encouraging, but maintenance records are stronger evidence.

Precision production also depends on measurement discipline. Confirm that the supplier uses calibrated gauges, coordinate measuring machines, vision systems, or suitable inspection tools. Review how operators record first-piece checks and in-process measurements. Traceable records should connect material batches, mold changes, machine settings, and inspection results. A small missing record can become a large investigation later.

Ask to see a sample run under normal production conditions. Laboratory samples can look excellent. Factory output tells a different story. Discuss preventive mold maintenance, spare components, and response plans for process drift. I have found that suppliers often describe automation better than they manage it. That deserves careful questioning. Reliable answers should be specific, documented, and repeatable.

How to Choose Precision Injection Molding Suppliers in 2026? — Assess Supplier Capabilities and Production Equipment
Category Evaluation Dimension Practical Reference Benchmark Recommended Verification Evidence Suggested Weight
Quality System Quality management certification A current ISO 9001 certificate issued by an accredited certification body. For medical-device work, ISO 13485 may also be required by the project or regulatory pathway. Certificate scope, validity date, issuing body, audit status, and site address should match the proposed production location. 10%
Dimensional Capability Process capability for critical dimensions For stable, well-controlled molding processes, a target of Cpk ≥ 1.33 is commonly used for critical characteristics; Cpk ≥ 1.67 may be specified for higher-risk features. Recent capability studies using production-intent tooling, material, machine, inspection method, and sample size. 15%
Molding Equipment Machine range and suitability Equipment should cover the required shot size, clamping force, mold dimensions, tie-bar spacing, injection pressure, and material-processing temperature. The required clamping force must be calculated from projected part area, cavity pressure, and a safety factor. Machine list showing clamping force, maximum shot weight, screw diameter, platen size, tie-bar spacing, and installation year. 12%
Machine Control Repeatability and process monitoring Closed-loop control of injection speed, pressure, screw position, and mold temperature is preferred for precision applications. Critical process parameters should be digitally recorded and traceable. Process-monitoring screenshots, control-plan records, alarm limits, data-retention policy, and sample batch reports. 10%
Tooling Capability Mold design, construction, and maintenance The supplier should control mold-flow review, steel selection, cooling design, venting, ejection, dimensional inspection, preventive maintenance, and engineering-change management. Mold design review checklist, maintenance schedule, spare-part plan, tool-life records, and documented change-control procedure. 12%
Metrology Inspection equipment and measurement traceability Measurement systems should be suitable for the tolerance level. Common equipment includes calibrated CMMs, optical measurement systems, vision systems, surface-finish instruments, and calibrated gauges. Equipment register, calibration certificates traceable to national or international standards, measurement uncertainty data, and MSA results. 12%
Measurement Quality Gauge repeatability and reproducibility For many attribute or variable measurement studies, an R&R result below 10% of total variation is generally preferred; 10%–30% may be acceptable depending on risk and customer requirements. Recent Gage R&R studies for critical dimensions, including operators, parts, repetitions, and acceptance criteria. 8%
Material Control Resin identification, drying, and traceability Resin lots should be traceable from incoming inspection through molding and shipment. Hygroscopic materials such as polyamide, polycarbonate, and PBT require controlled drying based on the resin supplier’s processing specification. Material certificates, lot-control records, dryer temperature and dew-point logs, regrind limits, and material-change approval records. 8%
Production Stability Capacity, uptime, and delivery control Capacity plans should include available machine hours, mold-change time, preventive-maintenance downtime, staffing, and a documented production schedule. Capacity should be demonstrated under comparable product conditions. Capacity model, production-load report, preventive-maintenance records, on-time-delivery history, and contingency plan for equipment failure. 7%
Validation Process qualification and first-article approval For critical or regulated parts, production should include documented design review, mold qualification, process qualification, first-article inspection, and approval of the production control plan before full release. Validation protocol, approved process parameters, first-article report, control plan, inspection plan, and deviation records. 4%
Automation Robotics and secondary-process consistency Automated part removal, insert loading, vision inspection, trimming, assembly, or packaging can reduce variation when the automation is validated and maintained. Automation risk assessment, cycle-time data, error-proofing controls, maintenance records, and inspection-system challenge tests. 2%
Use these benchmarks as a supplier-screening framework. Final acceptance limits should be defined by the part drawing, material specification, regulatory requirements, risk analysis, and customer quality agreement.

Verify Quality Systems, Materials, and Process Controls

Choosing a precision injection molding supplier in 2026 requires evidence, not polished presentations. The ISO Survey 2023 recorded 1,265,216 ISO 9001 certificates worldwide. Certification helps, but it does not guarantee capable molding. Request the supplier’s quality manual, internal audit results, corrective-action records, and calibration history. Verify whether operators follow documented procedures during night shifts, not only during customer visits.

Material control deserves equal attention. PlasticsEurope reported global plastics production of 413.8 million tonnes in 2023. That scale increases the importance of resin identification and traceability. Ask for certificates of analysis, drying records, batch numbers, and approved substitution rules. During an audit, inspect labeled storage bins and moisture-control logs. One mixed resin lot can alter shrinkage, color, and dimensional stability. Small gaps become expensive.

Process controls should connect directly to part performance. Review cavity-pressure data, mold-temperature records, cycle-time trends, and first-article inspection results. Ask for capability studies using real production data, not selected trial samples. A reported Cpk above 1.33 is useful, but confirm measurement-system analysis first. Check how the supplier handles drift, tool wear, and rejected parts. In practice, even experienced teams miss an occasional trend. That is why reaction plans must identify owners, limits, containment steps, and verification dates. I would also compare three recent production lots before approving the supplier.

Compare Pricing, Lead Times, Capacity, and Supply Risks

How to Choose Precision Injection Molding Suppliers in 2026?

Price comparisons should begin with a complete cost model, not the mold quotation alone. Include resin, tooling maintenance, inspection, packaging, freight, and engineering changes. The U.S. Bureau of Labor Statistics publishes monthly producer price indexes for plastics and resins. Use these indexes to test whether quoted material costs remain realistic. A low unit price may hide expensive rework.

Lead time needs evidence. Ask for recent mold-build records, first-article approval dates, and average corrective-action time. The World Bank’s 2023 Logistics Performance Index evaluates customs, infrastructure, tracking, and timeliness on a one-to-five scale. Compare the supplier’s location and logistics route against these factors. A promised 25-day delivery means little without buffer planning.

Capacity claims also require proof. Review machine tonnage, validated cavity counts, utilization, maintenance logs, and backup equipment. UNCTAD’s Review of Maritime Transport 2024 states that more than 80% of global merchandise trade by volume moves by sea. That creates exposure to port congestion, route disruption, and container shortages. Request dual-source plans for critical resins and standardized inserts. I would not trust a perfect quotation. Supplier audits can also miss overtime fatigue, weak traceability, or overloaded inspection teams. Ask for production data from comparable parts, then verify it through sample orders and measured capability results.

This anonymous 2026 benchmark compares common precision injection molding supplier profiles. Scores are normalized to 100, where a higher score indicates stronger performance: lower quoted pricing, shorter lead times, greater validated production capacity, and lower supply risk. Pricing and lead-time scores should be confirmed through a formal RFQ, while capacity and risk should be verified through audits, quality records, and business-continuity documentation.

Qualify the Supplier Through Audits and Prototype Testing

In 2026, supplier qualification should begin with evidence, not attractive capability lists. An on-site or remote audit should examine the production floor, inspection records, and change-control process. Ask how operators trace resin lots, machine settings, and inspection results. Review calibration dates for gauges and measurement systems. Check whether nonconforming parts receive documented root-cause analysis. A certificate helps. It does not prove daily discipline. Experienced auditors should compare written procedures with actual operator behavior, because gaps often appear beside the molding machine.

Prototype testing should use production-intent materials, tooling, and process conditions whenever possible. Otherwise, results may flatter the supplier. Define critical dimensions, cosmetic limits, tolerances, and test methods before sampling. Measure parts at several cavity locations and after conditioning, not only immediately after molding. Functional tests should reflect real loads, temperatures, and assembly forces. Record warpage, sink marks, flash, cycle time, and scrap. Keep the failed pieces. They often reveal more than a polished report.

During the audit, request a pilot run with traceable samples and independent measurement review. Compare the supplier’s data with your own measurements. Investigate differences without assuming bad intent; measurement systems can disagree. A supplier should explain process capability, corrective actions, and escalation contacts clearly. I would not approve a source after one successful batch. That is tempting, but incomplete. Repeated samples and transparent records provide stronger confidence than a perfect presentation.